Small-section extrusion
Small cross-section aluminum profiles for compact designs. Send the section drawing, alloy, wall thickness and required length for a feasibility review.
Products · 06
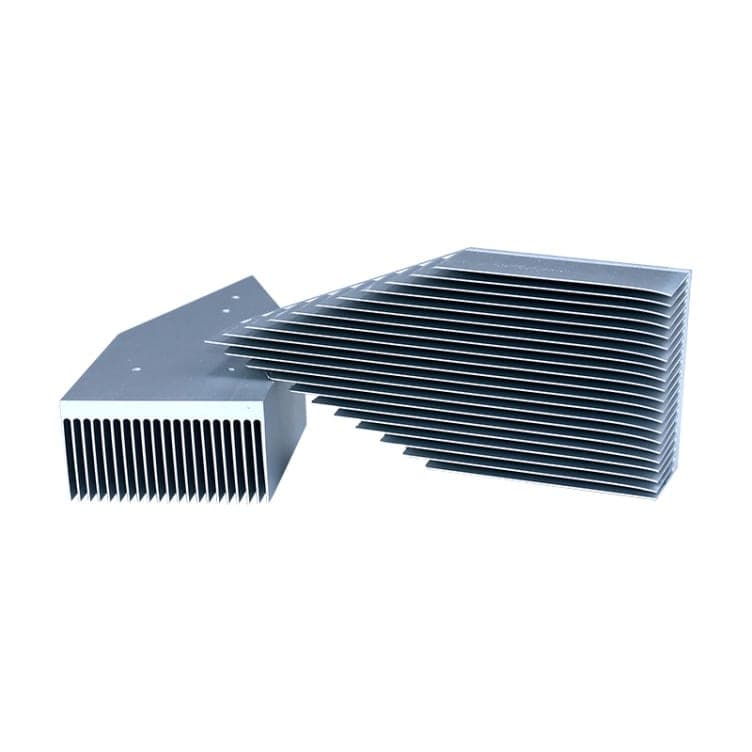
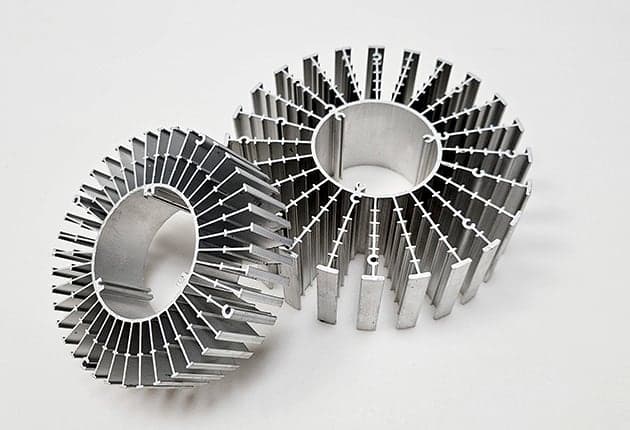
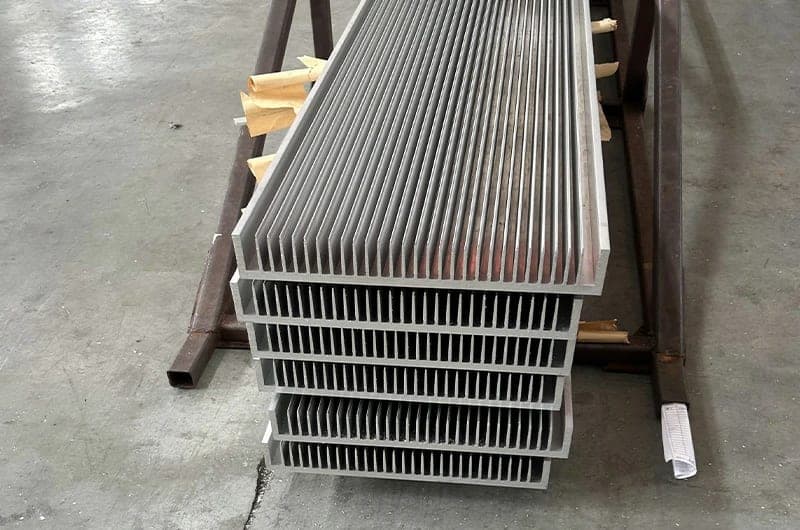
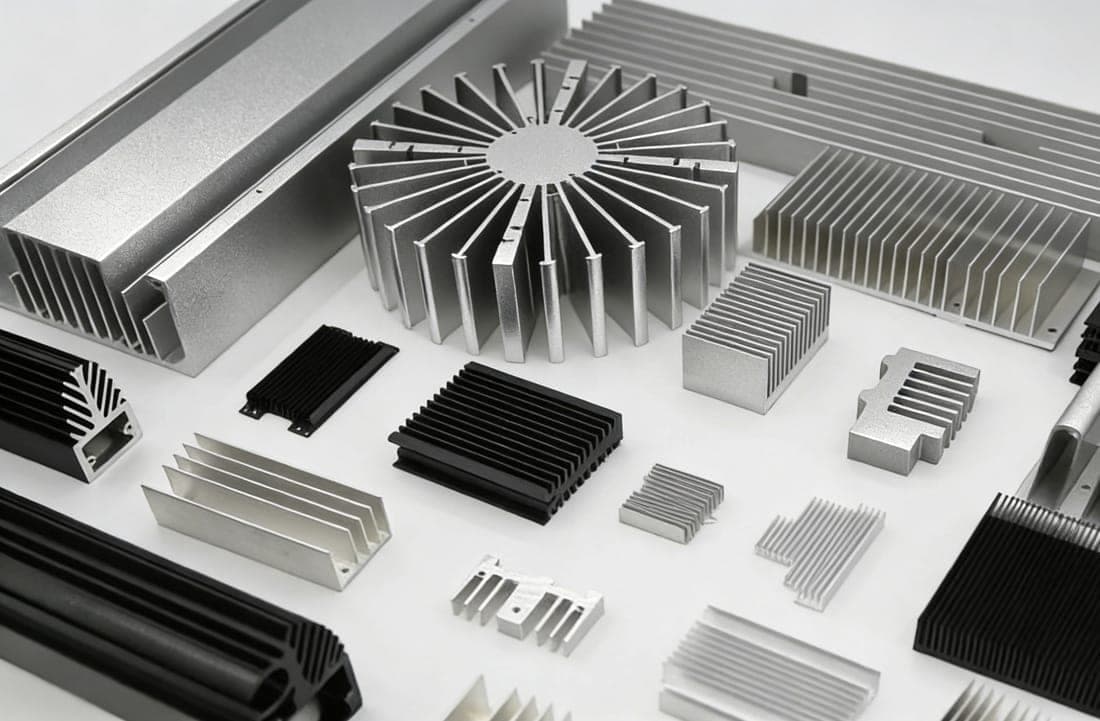
Source aluminum heat sink extrusions to your profile drawing, with secondary machining assessed for the finished component. Share fin geometry, base thickness, cut length and mounting requirements so we can review extrusion feasibility and quote the agreed scope.
Order aluminum profiles and combine the operations your application requires in the same quotation.
Small cross-section aluminum profiles for compact designs. Send the section drawing, alloy, wall thickness and required length for a feasibility review.
Blue, red, yellow, green, purple and black color options for small-batch projects. Specify the quantity per color and provide a color sample or reference.
Cutting, hole milling, drilling, welding and stretch bending can be quoted with your profiles. Include hole positions, bend geometry and assembly requirements.
Minimum section size, wall thickness, batch quantity and processing feasibility are confirmed from your drawing. Anodized shades depend on alloy, surface condition and sample approval; white finishes require confirmation of the finishing process.
For your quotation: section drawing · quantity by profile and color · cut lengths · machining or bending drawing · finish reference.
01Have these ready
Six things that turn a slow quote into a fast one.
02Where it's used
Sinks for inverters, drives and PSUs, machined for the device footprint.
Housing-and-sink sections for high-output LED modules.
Faced, drilled and tapped to your mounting drawing, ready to bolt on.
APPLICATION FOCUS
In a dense AI rack the heat sink stops being a commodity and becomes part of the device design: the extrusion route, fin form and machined interface get decided as one package, early.
An extruded sink wins when the fin section repeats along the length and volume matters. Once the fins get taller and tighter than extrusion aspect ratios allow, skived or bonded fins — or a CNC-milled cold plate — take over. Send the section and the duty; we will tell you which route fits, and we machine the mounting interface on either one.
03Specifications
| Parameter | Working range |
|---|---|
| Alloy grades | 6063 / 6061 |
| Temper | T5 / T6 |
| Fin geometry | to your drawing |
| Base / fin thickness | from 0.7 mm (0.3 mm on small sections →) |
| Machining | Cut, drill, tap, flatness |
| Dimensional tolerance | to EN 12020 / ±0.1 mm |
| Surface finish | Mill / Black anodized |
04Three confirmations before production
Fin height, spacing and base thickness affect extrusion feasibility. Send the section drawing, preferred alloy and application requirements. Manufacturing feasibility and thermal performance are separate checks; final thermal validation should use your intended assembly and operating conditions.
Mark flatness requirements, hole positions, thread sizes and any finish exclusions on mounting surfaces. Cutting, facing, drilling, tapping and finishing are assessed per drawing, with production arranged through our own and partner factories.
Machining and surface treatment are coordinated according to project requirements — CNC & machining · Finishing.
05Quality & certification
ISO 9001:2015 / GB/T 19001-2016
ISO 14001:2015 / GB/T 24001-2016
Issued by Shanghai Sailway Certification Co., Ltd. — accredited under CNAS / IAF MLA.
These certificates are held by our manufacturing plant.
Full stamped certificates are available on request. Numbers can be verified with the issuer or through CNAS.
06Frequently asked questions
Send the cross-section and required lengths. We review fin geometry, alloy and tooling feasibility before confirming whether the section can be extruded as drawn.
Yes, these operations can be assessed with the profile quotation. Include the hole pattern, thread specification and mounting-face requirements; the quotation will state the agreed machining scope.
No thermal improvement is guaranteed by the finish alone. Specify the required finish and mounting-surface conditions, and validate thermal performance in the intended operating environment.